1. Basic Mold Structure

Framework
System
Mold
Base
The
main body carrying all components(fixed plate, moving plate, support plate,
ejector plate, bottom plate,etc.)
Guide
Post,Guide Bushing
Locate
the fixed and moving halves, ensuring mold closing precision
Support
Pillar
Prevent
template deformation under pressure
Return
Pin/Spring
Allow
the ejection system to return when opening the mold
|
Molding System |
|
|
Mold Core(Cavity/Core) |
Determine the shape of the product. The material is P20/NAK80/S136. |
|
Slider,Lifter |
Handles product undercuts |
|
Insert |
Locally replaceable wear-resistant or special functional components |
|
Feeding System |
|
|
Gate |
The final narrow opening for plastic to enter the mold cavity, determining shear and appearance |
|
Runner |
The delivery channel from the injection nozzle to the gate |
|
Sprue Bushing |
The entrance in contact with the injection machine nozzle |
|
Cold Slug Well |
Catch cold slugs to prevent gate blockage |
|
Hot Runner |
Keep the runner in a molten state, producing no sprue waste, commonly used for large volume production |
Cooling
and Ejection
Cooling
Channel
The
core of mold temperature control, directly affecting cycle time and warpage
Ejector
Pin/Ejector Sleeve
Ejects
the finished product after the mold opens
Ejector
Plate, Bottom Plate
Drive
the action of the ejector pin assembly
Venting
System
The
exhaust of air in the mold cavity; poor venting leads to short shots or burn
marks
2. Mold Core and Steel Materials

3. Common Plastic Materials

4. Introduction to Plastic Molding


5. Common Defects of Plastic Molding

|
Short Shot |
|
|
Possible Causes |
Insufficient material amount, material/mold temp too low, slow injection speed, poor venting, runner or gate too small |
|
Countermeasures |
Increase material amount, raise temperature, increase speed, improve venting(add vent grooves), enlarge gate |

|
Warpage |
|
|
Possible Causes |
Uneven cooling, uneven wall thickness, differential shrinkage, excessive holding pressure, unbalanced ejection |
|
Countermeasures |
Balance cooling channels, adjust wall thickness design, lower mold temp, adjust holding pressure curve, check ejection system |


|
Silver Streak/Fogging |
|
|
Possible Causes |
Plastic not sufficiently dried, material contamination, shear overheating, material temp too high |
|
Countermeasures |
Strengthen drying, check material cleanliness, lower injection speed, raise mold temp, lower material temp if necessary |

|
Sticking |
|
|
Possible Causes |
Insufficient draft angle, rough mold surface, insufficient cooling, improper ejection positions |
|
Countermeasures |
Increase draft angle(≥1°),polish mold surface, check cooling channels, reconfigure ejector pins |

|
Weld Line |
|
|
Possible Causes |
Insufficient temperature at convergence multiple plastic flows, mold temp too low, poor venting, additive effects |
|
Countermeasures |
Raise mold and material temp, increase venting, adjust gate position to avoid appearance surfaces, switch to material with better flowability |
|
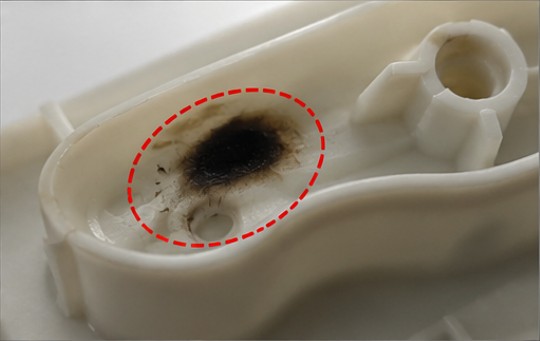
Burn Mark |
|
|
Possible Causes |
Poor venting, shear overheating, material left in barrel too long and burned, gate too small |
|
Countermeasures |
Add vent grooves, lower injection speed, purge barrel, enlarge gate, check hot runner temperature |
© 2026 ShengYih Technologies Co., Ltd All rights reserved.